ACCURACY
Trueness plus precision
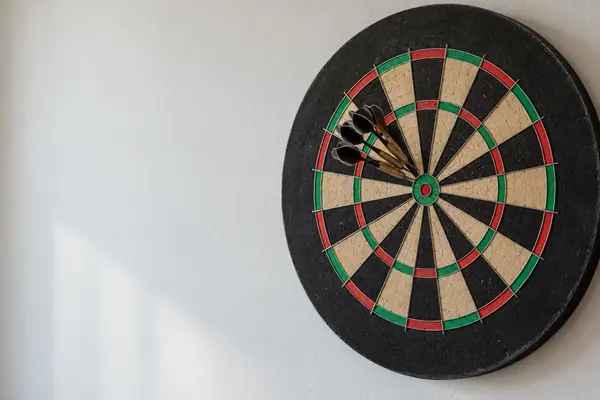
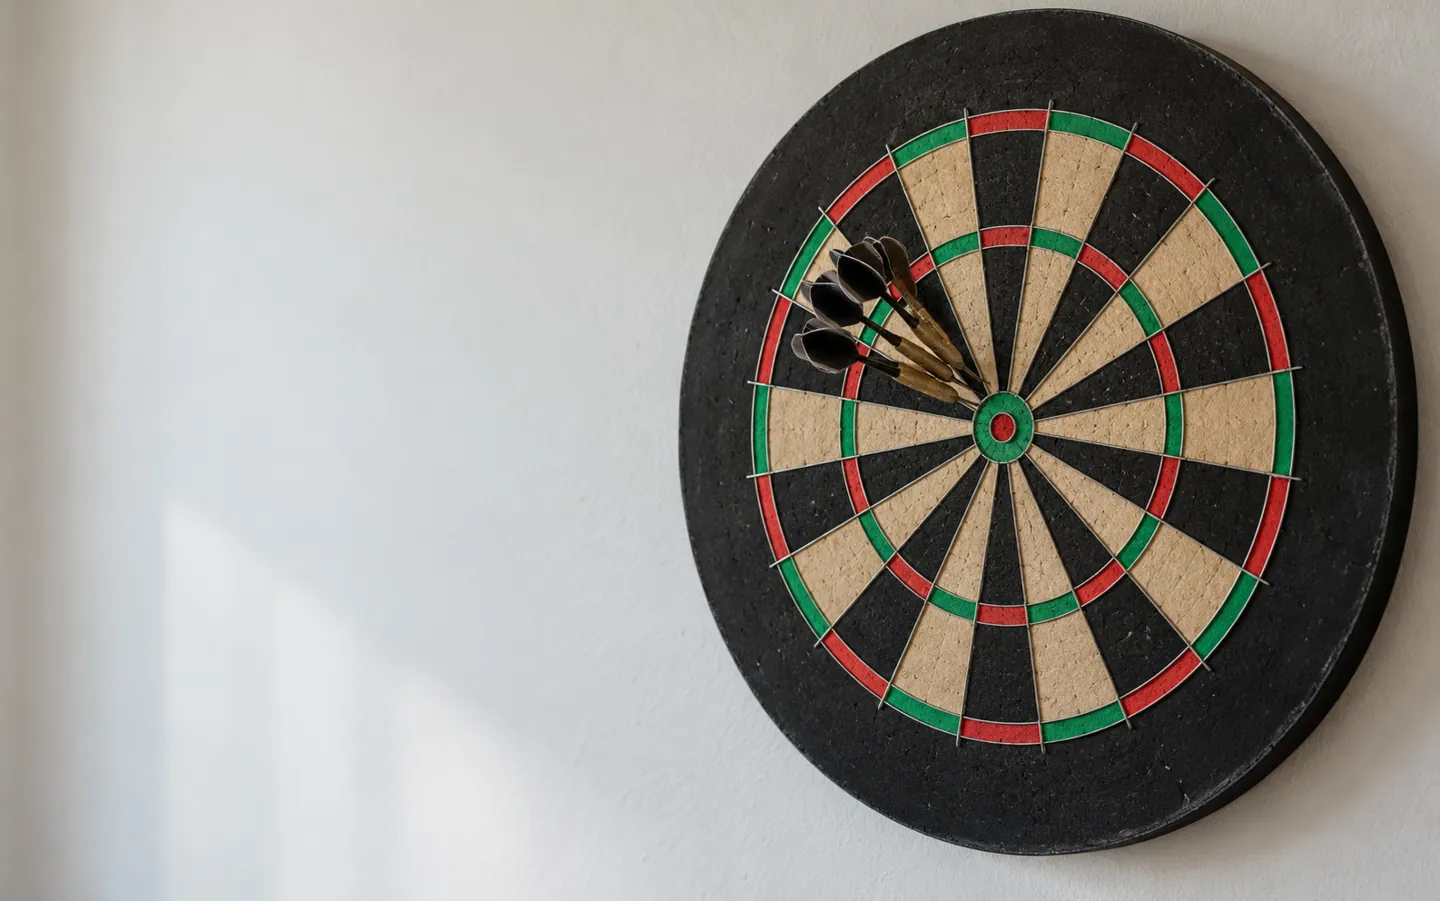
The UK's National Physical Laboratory puts it simply: high accuracy is a combination of high precision and high trueness. Darts can be tightly grouped and still miss the bullseye.
Check a processMEASUREMENT, MADE PLAIN
Every made thing has a number it aims for, and a range it must stay inside.
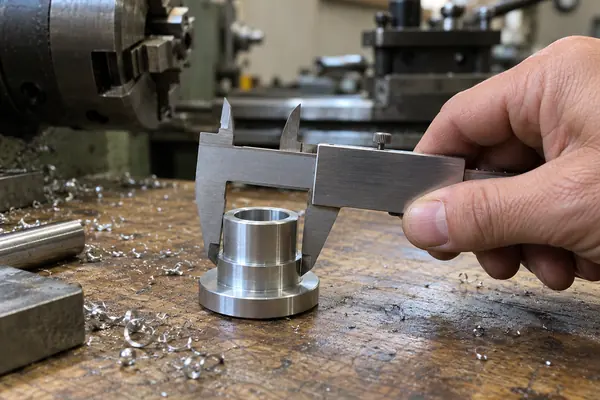
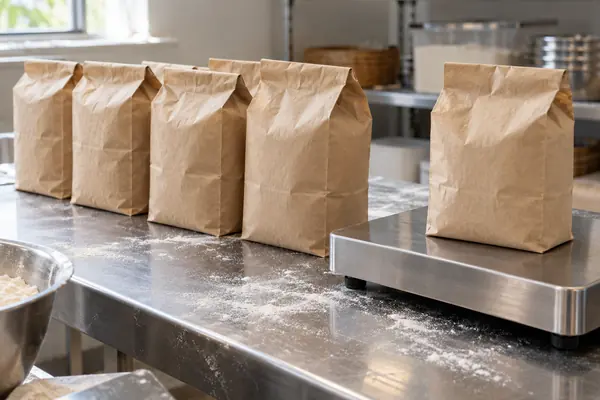
A bolt, a bag of flour or a bottle of juice is made to a target, with limits either side. Whether a maker really hits that target comes down to two separate questions: are the results centred on it, and are they close to each other? Measurement scientists have agreed words for both.
0.27% outside ±3σ
THE SHORT ANSWER
Centred? Consistent?
And inside the spec?
ACCURACY
The UK's National Physical Laboratory puts it simply: high accuracy is a combination of high precision and high trueness. Darts can be tightly grouped and still miss the bullseye.
Check a processSPECIFICATION
A spec gives a target and upper and lower specification limits. Capability indices such as Cp and Cpk compare that allowed width with how much the process actually varies.
See the numbersIN THE SHOPS
Under the UK's average system, packs must not be less on average than the stated quantity, and no pack may be short by more than twice the tolerable negative error.
The packers' rulesA QUICK CAPABILITY CHECK
Pick a Cp value for a well-centred process. The bar shows how many parts would land outside the specification limits.
Figures from the NIST/SEMATECH e-Handbook of Statistical Methods. They assume normally distributed results centred on the target; a process that drifts off-centre does worse.
TWO NUMBERS WORTH KNOWING
One figure from the factory floor,
one from the supermarket shelf.
0.27%
Share of normal results beyond ±3 standard deviations
For normally distributed data, 0.00135 lies beyond 3σ in each direction, or 0.0027 in both. That is why control charts usually draw their limits at ±3σ around the centre line.
3-SIGMA LIMITS · NIST
9 g
Tolerable negative error for a pack between 200 g and 300 g
A 250 g pack falls in the 200 to 300 g band, where the TNE is 9 g. Only a limited proportion may be short by more than that, and none by more than twice it.
PACKED GOODS · OPSS
Sources: NIST/SEMATECH e-Handbook, section 6.3.1, What are Control Charts?; Weights and Measures (Packaged Goods) Regulations 2006: Great Britain guidance, Office for Product Safety and Standards.
THE UK AVERAGE SYSTEM
Automatic filling always varies a little. The average system sets tolerances for that variation, so shoppers are protected against short measure and packers can still run their lines.
The actual contents must not be less, on average, than the nominal quantity printed on the pack.
The proportion of packs short by more than the tolerable negative error must stay below a specified level.
No pack may be short by more than twice the tolerable negative error, whatever the average.
The optional ℮ mark is the packer's declaration that the contents comply with the average system. Trading Standards enforce the rules.
CONTROL LIMITS ARE NOT SPEC LIMITS
Specification limits come from the design: what the part or pack must be. Control limits come from the process itself, set so that almost all points fall inside them while it stays in control. A point outside them is a signal to look for a cause.
In the US, control limits are usually set at 3 standard deviations. NIST notes that statisticians in the UK generally prefer probability limits, such as 0.001 in each direction, which for normal data sit very close to the 3σ lines.
Questions
Precision is how close repeated results are to each other. Trueness is how close their average is to the reference value. NPL says high accuracy combines both.
NPL calls that a myth: precision relates to the measurement results, not to the instrument used to find them.
Cp compares the width between the specification limits with six standard deviations of the process. Cpk also accounts for how far the average sits from the centre, so it is never larger than Cp.
NIST says most capability estimates are valid only with a large enough sample, generally thought to be about 50 independent data values, and they assume normally distributed data.
Yes, within limits. Under the UK average system the average must reach the stated quantity, few packs may fall short by more than the TNE, and none by more than twice it.
Sources
ABOUT THIS NAME
targetspec.com is part of the DoodleSale portfolio. It isn't in an auction right now, but you can ask about leasing it.